Soft vs Metal-Backed Hydraulic Wiper Seals: A B2B Selection Guide for Replacement Kits
Choosing between a soft wiper seal and a metal backed wiper seal is rarely about which part is “better”. For seal distributors, hydraulic repair shops, forklift and construction-equipment fleets, and the procurement staff who write the purchase orders, the real question is narrower: which wiper can survive the housing groove, the rod condition, and the installation method that exist on one specific machine, and which one can be verified before a wiper seal replacement kit leaves the warehouse. Recent maintenance chatter in forklift lift-cylinder repair threads and hydraulic repair forums keeps circling the same practical split between soft and metal-backed wipers, which is a useful reminder that the decision is situational rather than categorical. This guide frames a hydraulic wiper seal comparison around the checkpoints that actually appear on an RFQ: groove geometry, contaminant type, rod end features, mating rod seal, receiving inspection, sample testing, and the fields a supplier needs to quote accurately.
Why Soft and Metal-Backed Wipers Are Not Interchangeable
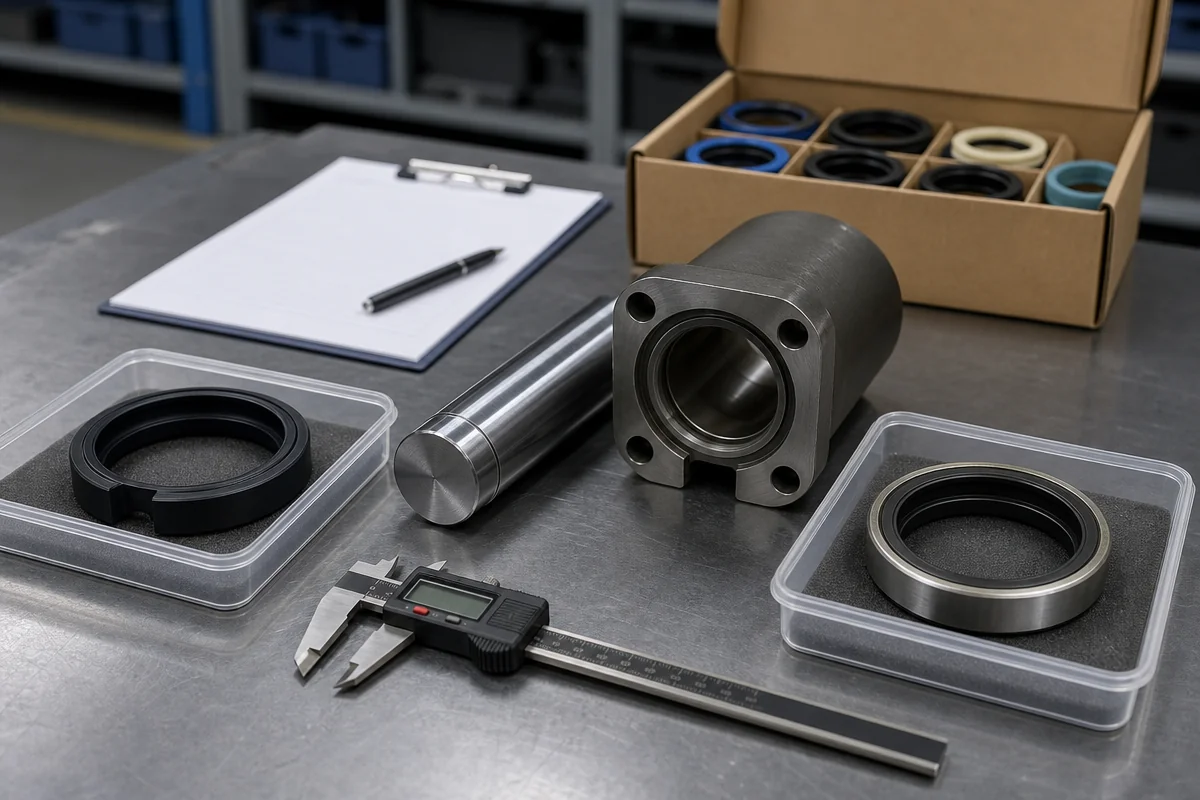
A wiper (also called a scraper or excluder) sits at the rod end of a cylinder and its job is to keep external contamination off the rod before it is drawn inward past the rod seal. Two wipers that share the same nominal rod diameter can still behave very differently once they are in the machine, because the retention method differs: one relies on a flexible lip compressed into an elastomeric groove, the other relies on a rigid case pressed into a machined bore. Swapping one for the other without checking the housing usually ends in a part that either will not seat, will not stay seated, or damages the rod during installation.
That is why “just match the rod diameter” is not a rod wiper seal selection method. Rod diameter is the starting filter, not the answer. The answer comes from the housing drawing, the rod end drawing, the contaminant profile, and the confirmed part identity of whatever came out of the machine.
What Each Wiper Actually Is
A soft wiper seal is typically a molded elastomer or polyurethane body with one or more flexible lips and no rigid reinforcing case. It is retained by the groove itself — by compression, by a snap-in profile, or by a cover plate depending on the design — and it generally installs by hand, by rolling the lip over the rod end, or with a simple tapered sleeve. Because the body is flexible, it tolerates modest housing variation and is easier to seat in worn or re-machined grooves, but it is also more exposed to mechanical damage from impact, ice, and sharp rod-end features.
A metal backed wiper seal carries a rigid metal case around or behind the sealing lip. The case carries the press-fit load into the housing bore, so the wiper holds its shape under side load and resists deformation from external impact better than an unsupported lip. In exchange, the metal case demands a housing bore that is round, correctly sized, and free of damage, plus a proper lead-in chamfer so the lip and case are not cut or shaved as the seal passes over the rod end. Both families can appear in the same machine family, and some cylinders use a combination of a metal-cased wiper with a secondary lip. Which one belongs in a given position has to be confirmed with the supplier, the housing drawing, and the application data.
Housing Groove and Retaining Geometry
The single most common reason a wiper seal replacement kit fails at installation is that the housing was assumed rather than measured. For a soft wiper seal, the checkpoints are groove width and depth, the presence and condition of the retaining shoulder or cover plate, and whether the groove walls are still square after years of service. A flexible lip can absorb some of that variation, but a badly worn groove that has lost its shoulder will not retain a soft wiper reliably.
For a metal backed wiper seal, the checkpoints shift to the bore: bore diameter and roundness, counterbore depth and squareness, corner radius, and the lead-in chamfer angle and finish at the rod end of the housing. A metal case that is pressed into an out-of-round or scored bore may hold dimensionally and still leak past the case-to-bore joint. Re-machined housings are a particular risk, because the new bore may be dimensionally acceptable for the seal while the counterbore depth and chamfer no longer match the original drawing.
Before committing to either family, capture the housing dimensions from the drawing or from a clean measurement, note any repair or re-machining history, and confirm the retention method with the supplier. Where the housing condition is unclear, that uncertainty belongs in the RFQ, not in an assumption on the shop floor.
Contamination Exposure: Match the Seal to the Actual Contaminant
“Dirty environment” is too coarse a label for choosing a wiper. What matters is the specific contaminant the rod meets on the return stroke: dry abrasive dust and fines, wet mud and slurry, wash-down water, ice and frozen debris, metal chips and weld spatter, or process residue such as fertilizer, salt, or food-grade powders. Each of these loads the wiper differently.
A soft wiper seal with a flexible lip can follow rod runout and small surface irregularities and is often chosen where the contaminant is fine and the rod end is relatively protected. A metal backed wiper seal tends to hold its lip geometry under heavier, more violent exposure — impact from debris, packed mud, or ice — because the case does not deform the way an unsupported elastomer body can. The trade-off is that a rigid case concentrates load at its own contact band, so bore damage or a poor chamfer can cause the seal itself to become the wear source. In practice, a hydraulic wiper seal comparison should be run against the contaminant list plus the rod surface condition, and the final selection confirmed with the supplier against the application data rather than against a generic environment label.
Rod End Design and Installation Risk
Wiper damage during installation is common and usually avoidable. The features that matter are the rod end threads, the chamfer or radius at the rod tip, any cross-drilled ports, welded yokes or eye ends, keyways, and the presence of a step where the rod transitions to the piston. Sharp edges cut lips; loose threads shave them; a missing or too-small chamfer turns a two-minute installation into a scrapped seal.
For a soft wiper seal, the risk is a torn or rolled lip and a lip that has been pushed through the groove during seating. For a metal backed wiper seal, the risk is a shaved lip or a case that has been forced past the chamfer and has taken bore material with it. Both cases call for the same discipline: protect the rod end with a sleeve or tape where possible, use an installation guide, confirm the correct chamfer from the drawing, and dry-fit the seal before final seating if the housing condition is questionable. If the rod end cannot be protected in the field, that constraint is a reason to re-examine the wiper family choice with the supplier rather than to force the original part in.
The Mating Rod Seal in the Same Kit
Wipers do not work alone. The rod seal behind them defines the pressure and fluid boundary, and in many cylinders a buffer or backup element sits between them. That means the wiper family choice has to be made together with the rod seal, not after it. If the kit drawing specifies a soft wiper seal, moving to a metal backed wiper seal changes the stack height in the housing and can change how the rod seal is loaded and retained.
Two rules keep this practical. First, treat the kit as a set: part numbers, revision, and element order come from the kit drawing, and individual elements should not be substituted from a “similar” kit that happens to share a rod diameter. Second, when a substitution is proposed, state clearly which element is changing, why, and what the supplier confirms about the revised stack, groove fit, and fluid compatibility. Fluid compatibility in particular is application-specific — hydraulic oil grades, biodegradable fluids, water-glycol, and high-water-content fluids behave differently against wiper lip materials — and must be confirmed with the supplier against the actual fluid in use.
Receiving Inspection, Sample Testing, and Quarantine Rules
Receiving inspection is where a distributor or fleet earns back the cost of a bad batch. Useful, low-cost checks include: confirming the kit part number and revision against the purchase order and the kit drawing; comparing element count and element identity against that drawing; checking case squareness and lip profile on metal-backed parts; checking for tears, cuts, or molding flash on soft parts; and verifying that packaging has not deformed or crushed the elements. Dimensional checks should follow the drawing’s stated values rather than an assumed standard, and any measurement outside the drawing tolerance should be treated as a nonconformance, not a rounding issue.
Sample testing means installing one unit from the batch in a controlled situation and observing behaviour before the rest of the batch is released to customers or put into fleet service. What is observed, for how long, and against what acceptance criteria are all application-specific and should be agreed with the supplier and recorded — do not assume a universal pass/fail figure. It also helps to keep a written rule for what happens to a questioned batch while the supplier is being consulted, so that shop-floor urgency does not turn a “hold” into a “fit it anyway”.
Soft vs Metal-Backed Hydraulic Wiper Seal Comparison Table
| Selection factor | Soft wiper seal | Metal backed wiper seal |
|---|---|---|
| Retention method | Groove compression, snap-in profile, or cover plate; no rigid case | Rigid case pressed into a machined bore or counterbore; confirm housing drawing |
| Housing checkpoints | Groove width, depth, retaining shoulder condition | Bore diameter, roundness, counterbore depth and squareness, corner radius |
| Lead-in chamfer | Tolerant of minor variation; lip can still be rolled or torn | Critical; an undersized chamfer can shave the lip or case |
| Installation method | Usually hand or sleeve assisted; watch for lip roll-through | Press or controlled seating into the bore; use a guide and confirm seating depth |
| Contaminant behaviour | Follows rod runout and light surface variation; lighter exclusion band | Holds lip geometry under impact and packed debris; load concentrated at its own band |
| Rod condition sensitivity | More forgiving of slight runout; still sensitive to scoring and burrs | Sensitive to bore damage and out-of-round housings; case-to-bore joint is a risk point |
| Removal and re-use | Generally removed without damaging the groove | Removal can mark the bore; inspect the bore before fitting a replacement |
| Before ordering | Confirm groove drawing, retention method, and contaminant with supplier | Confirm bore drawing, chamfer, seating depth, and fluid with supplier |
Decision Table: Which Direction to Start From
Use the table below as a starting filter, then confirm every line with the supplier, the assembly drawing, and the application data. The right-hand column is the part that prevents a wrong substitution.
| Application signal | Starting direction | What must be confirmed |
|---|---|---|
| Original part is a metal-cased wiper and the housing bore is in good condition | Stay with a metal backed wiper seal | Bore and counterbore dimensions, chamfer, seating depth, case markings led by kit drawing |
| Housing re-machined, or groove width and shoulder condition uncertain | Review a soft wiper seal option | Post-machining groove and retention method, rod runout, contaminant profile — confirm with supplier |
| Rod end exposed to impact, packed mud, ice, or demolition debris | Favour a metal backed wiper seal design with a secondary lip if the drawing permits | Impact direction, rod protection, housing fit, fluid compatibility — confirm with application data |
| Fine abrasive dust or clean workshop environment with protected rod | Soft wiper seal is often sufficient | Rod surface finish, lip material against the fluid, groove retention |
| Wash-down, salt, fertilizer, or food-grade powder exposure | Decide by chemistry and cleaning method, not by shape alone | Actual fluid and cleaning agents, wiper lip material, housing material and finish — confirm with supplier |
| Replacement kit cannot be identified with certainty from the machine | Do not substitute; identify first | Machine plate data, cylinder part number, kit drawing revision, photograph of the removed wiper |
Normal, Confirm, or Quarantine? A Shop-Floor Judgment Table
Shop-floor staff need a fast rule for what to fit, what to question, and what to hold back. The categories below are process categories, not acceptance limits; the actual acceptance values come from the drawing and from the supplier.
| Observation | Category | Action |
|---|---|---|
| Kit part number, revision, and element count match the kit drawing | Normal | Release for use; file the packing slip and drawing reference |
| Soft lip shows light surface bloom or dry appearance, no cuts or tears | Normal | Note the condition; keep the element in its original packaging until fitting |
| Metal case shows nicks, out-of-round, or a damaged seating face | Quarantine | Detain the batch, raise a nonconformance, and consult the supplier |
| Two different lip materials or shapes shipped loose in one bag | Quarantine | Do not mix; obtain a corrected kit and a written identity confirmation |
| Label or marking differs from the kit drawing revision | Confirm with supplier | Hold until the revision is reconciled in writing |
| Housing bore or groove shows scoring or a chamfer that does not match the drawing | Confirm with supplier | Re-measure against the drawing and ask whether the wiper family still fits the as-found housing |
| Fluid in the machine differs from the fluid recorded for the kit | Confirm with supplier | Verify material compatibility against the actual fluid before fitting |
| Sample unit installed on a trial cylinder for observation | Normal (controlled) | Record the observation method and criteria agreed with the supplier before the trial |
RFQ Fields: What Procurement Should Send
A complete RFQ shortens the back-and-forth and reduces the chance of a wrong-element kit being shipped. When requesting a wiper seal replacement kit, include the following where available, and mark anything that is unknown as unknown rather than estimating it.
- Machine identity: make, model, serial or fleet number, and the assembly the cylinder belongs to.
- Assembly and kit numbers: cylinder part number, existing seal kit number, and the revision of the kit drawing if known.
- Housing data: groove type, groove width and depth, bore diameter and condition, counterbore depth, corner radius, and lead-in chamfer — from the drawing where possible.
- Rod data: rod diameter, surface condition, runout, and any scoring or plating damage.
- Rod end features: threads, tip chamfer, ports, welded yoke or eye, keyways, and any step near the piston.
- Wiper family in the original build: soft wiper seal, metal backed wiper seal, or a combination, plus a photograph of the removed part with its markings.
- Contaminant profile: the specific media the rod meets — dust and fines, mud, ice, wash-down, chips, or process powders — and how the machine is cleaned.
- Fluid and operating context: fluid type in use, and the machine’s duty cycle described in the customer’s own terms rather than as an assumed rating.
- Quantities and usage pattern: units per service event, expected order pattern, and whether the kit is for stock or for a specific repair.
- Documentation needs: which documents the buyer requires — confirm availability and format with the supplier rather than assuming a standard package.
- Handling constraints: how elements will be transported and stored at the destination, so the supplier can advise appropriate packaging.
FAQ: Soft vs Metal-Backed Wiper Seals
Can I replace a soft wiper seal with a metal backed wiper seal if the rod diameter is the same?
Not on rod diameter alone. The metal case needs a compatible bore, counterbore depth, corner radius, and lead-in chamfer, and the change can affect the rod seal stack. Confirm with the supplier against the housing drawing before substituting.
Which wiper type lasts longer?
There is no universal answer, and no supplier should quote a service life without the application context. Contaminant type, rod condition, housing condition, fluid, duty cycle, and installation quality all influence service outcome. Confirm expectations with the supplier and with the application data for that machine.
My housing was re-machined. Does that change the wiper family?
It can. Re-machining may change bore diameter, counterbore depth, and groove geometry, which affects both families differently. Provide the post-machining measurements and the original drawing to the supplier and ask them to confirm fit for the as-found housing.
Is a metal-backed design always the better choice in dirty conditions?
Not always. Metal cases resist deformation from impact and packed debris, but they concentrate load and depend on good bore condition. Where the housing is worn or the rod runs out, a soft wiper seal may fit the actual machine better. The right answer is application-specific and must be confirmed.
What should I check when a kit arrives?
Confirm part number, revision, and element identity against the kit drawing; inspect soft lips for cuts, tears, or flash; inspect metal cases for nicks or out-of-round; and verify packing has not crushed the elements. Any deviation is a nonconformance to raise with the supplier, not something to fit anyway.
Do I need to test a sample before releasing a batch?
For a new source, a new revision, or a repeat problem, a controlled sample installation is a reasonable step. The observation method, duration, and acceptance criteria should be agreed with the supplier in advance and recorded, because they are specific to the application rather than universal.
How do I compare wiper options honestly?
Run the comparison on the same five inputs for each candidate — housing geometry, contaminant profile, rod and rod-end condition, mating rod seal stack, and fluid compatibility — and ask the supplier to confirm each against the drawing. A hydraulic wiper seal comparison that skips any of these inputs is incomplete.
Can I mix brands or revisions inside one kit?
Do not assume interchangeability between revisions or brands even when the dimensions appear close. Element identity should follow the kit drawing; any deviation needs written confirmation from the supplier.
Related Reading and Next Step
Two companion references go deeper on adjacent validation topics: wiper seal selection with contaminant exclusion in mind covers contamination-driven choices in more detail, and seal kit dimension and tolerance validation covers how to check a kit against its drawing. Where batch identity and documentation matter to your process, see seal kit traceability and batch control.
If you are evaluating a rod wiper seal selection for a specific cylinder, or you need a wiper seal replacement kit quoted for a fleet or a distribution programme, send the RFQ fields above to DJF Seal through the website contact channel. Include photographs of the removed wiper, the kit drawing reference, the housing and rod measurements, and the fluid in use. Our team will confirm the relevant points — housing fit, wiper family suitability, mating rod seal stack, and fluid compatibility — against your drawing and application data, and will tell you plainly which details still need to be verified before a replacement kit is released.
 Excavator Center Joint (Swivel Joint) Seal Kits: Internal Cross-Port Leakage Troubleshooting, PTFE Step-Seal Selection & B2B Overhaul Guide
 Excavator Main Control Valve Seal Kits: Spool Leakage Troubleshooting, Material Selection & B2B Sourcing Guide
 Hydraulic Breaker Hammer Seal Kits: B2B Sourcing, Material Selection, and High-Frequency Shock Protection Guide
 Motor Grader Hydraulic Cylinder Seal Kits: A B2B RFQ and Selection Guide