Hydraulic Breaker Hammer Seal Kits: B2B Sourcing, Material Selection, and High-Frequency Shock Protection Guide
Introduction: Why Breaker Seal Kits Demand a Different Playbook
Hydraulic breaker hammer seal kits sit at the convergence of two of the most punishing forces in mobile hydraulics: extreme pressure spikes and relentless high-frequency impact. A breaker does not cycle like a smooth cylinder — it fires its piston between roughly 600 and 1,800 blows per minute, transferring a shock wave through the tool, the front head, and the piston-cylinder interface thousands of times per hour. Every one of those blows loads the sealing system with a rapid pressure pulse followed by an almost instantaneous decompression. Seal profiles that survive a standard excavator cylinder will fail within weeks in a breaker because the failure mechanism is not steady wear — it is fatigue, extrusion, and decompression damage driven by shock.
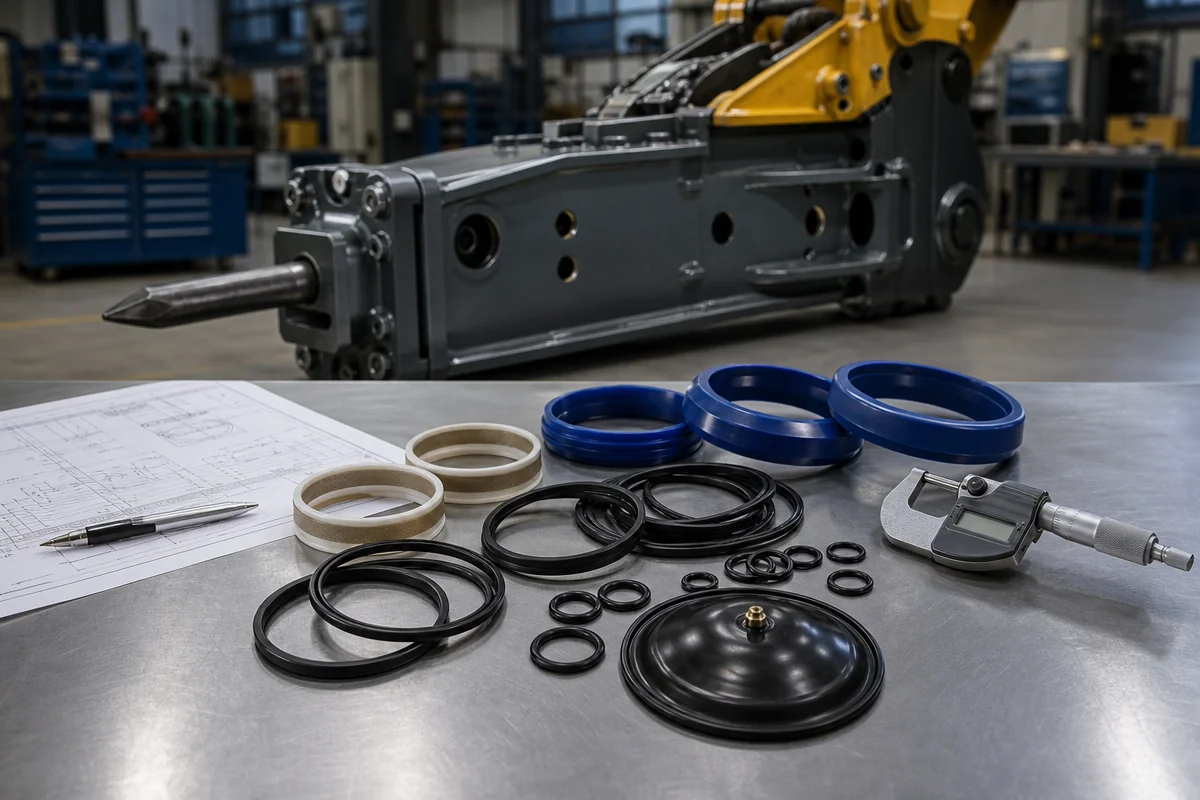
For B2B buyers — parts distributors, hydraulic repair workshops, and procurement managers at quarrying and demolition contractors — the breaker seal kit is a high-turnover consumable with an outsized influence on machine uptime. A single mismatched step seal can convert a planned seal refresh into a full piston replacement, and a batch of seals with inconsistent hardness can trigger repeat failures that damage your reputation far more than they damage the hammer. This guide maps the technical selection criteria and procurement controls that separate dependable breaker seal kits from generic substitutes.
How a Breaker Differs From a Conventional Hydraulic Cylinder
Understanding breaker sealing starts with the operating envelope. Three characteristics set it apart from any ordinary rod-and-piston application:
- Shock pressure spikes: Working pressure can peak well above the nominal system rating during each strike, and the seal must resist extrusion at these transient peaks rather than only at steady state.
- High cycling frequency: With up to 30 strikes per second, the piston seal sees a duty cycle hundreds of times higher than a typical cylinder, accelerating fatigue and heat build-up.
- Gas chamber pressurisation: Nitrogen-backed accumulators and gas chambers rely on elastomers and diaphragms that must hold charge for long intervals while being cycled by every blow.
Because these conditions coexist, a breaker seal kit is not a single product but an engineered system of matched components. Selecting them as a set — rather than replacing one seal at a time — is the first rule of reliable breaker maintenance.
Anatomy of a Hydraulic Breaker Seal Kit: Components and Functions
A professional breaker repair kit groups the seals by the functional zone they protect: the piston-cylinder interface, the buffer region that absorbs recoil, the gas chamber that stores energy, and the wiper zone that keeps contamination out of the front head. The table below maps each component to its function and the operating pressure band it is designed to withstand. Buyers reviewing our full range of hydraulic seals will recognise this zoning pattern across hammer brands.
| Seal Component | Primary Function | Typical Operating Pressure Band | Shock Sensitivity |
|---|---|---|---|
| Piston Step Seal | Main dynamic seal at the piston-cylinder interface; contains the high-pressure working oil during each strike | Up to 350 bar peak / 160–220 bar working | Very high — first component to suffer extrusion and nibbling |
| Buffer Seal | Absorbs pressure peaks ahead of the main seal and dampens the shock wave before it reaches the primary sealing edge | 250–350 bar transient | Very high — designed as a sacrificial shock absorber |
| Gas Chamber O-Rings | Static sealing of the nitrogen gas chamber and accumulator connections to retain charge pressure | 10–40 bar gas, cycled by every blow | Moderate — vulnerable to compression set and gas permeation |
| Diaphragm | Separates gas from hydraulic fluid in the accumulator; flexes continuously to store and release strike energy | Gas side 10–40 bar, flexed at strike frequency | High — fatigue and cracking under repeated flexing |
| Heavy-Duty Wiper | Scrapes dust, rock fines, and debris from the exposed piston rod to protect internal seals from abrasion | Low pressure, high contamination exposure | High — abrasion resistance is the governing property |
Two practical takeaways follow from this layout. First, the buffer seal and the piston step seal are a matched pair: replacing one without the other leaves the remaining part to absorb shock it was not sized for. Second, gas chamber components fail quietly — a slow nitrogen leak degrades striking power before it produces an obvious oil leak, so they belong in every scheduled kit.
Material Selection Under Heavy Shock Loads
Material choice is where most breaker seal failures are either prevented or pre-programmed. Under shock loading, four properties dominate: extrusion resistance, elastic recovery, compression-set resistance, and thermal stability. No single polymer wins on all four, so a well-engineered kit mixes materials by function. The comparison below reflects how each candidate performs specifically in the breaker envelope.
| Material | Shock / Extrusion Behaviour | Temperature Range | Best-Fit Application | Limitations |
|---|---|---|---|---|
| High-grade PU (Polyurethane) | Excellent elastic recovery and abrasion resistance; resists nibbling better than most elastomers | −30 °C to +100 °C | Piston step seals, buffers, wipers | Hydrolysis risk in wet/high-temperature service; needs quality grade control |
| Bronze-filled PTFE | Highest extrusion and pressure resistance; low friction; near-zero compression set | −60 °C to +200 °C | High-pressure step seals and back-up rings at peak loads | Lower elasticity; requires an energiser or matched profile |
| FKM / Viton | Good compression-set resistance and thermal stability; reliable static sealing | −20 °C to +200 °C | Gas chamber O-rings, high-temperature static seals | Higher cost; limited low-temperature flexibility |
| NBR 90 Shore A | Hard, oil-resistant, cost-effective; moderate extrusion resistance | −30 °C to +100 °C | Static seals and general-purpose O-rings at moderate pressure | Higher compression set than FKM; degrades faster under sustained heat |
A balanced breaker kit typically pairs a bronze-filled PTFE step seal or a high-performance PU profile at the piston interface with FKM gas chamber O-rings and a hard PU wiper. Durometer (hardness) matters as much as polymer family: the dynamic seals in a breaker are usually specified harder than their cylinder cousins precisely to resist extrusion during the strike transient. When a buyer needs to replicate an original profile, the correct sequence is to measure hydraulic seals against the worn part and the housing before confirming a material, because a correct material in a wrong cross-section will still fail.
High-Frequency Shock: Failure Modes and Vibration Symptoms
In a breaker, the classic failure modes do not present the way textbook wear does. The dominant drivers are shock and vibration, so diagnosis has to read the machine’s behaviour, not only the removed seal. The following table links failure modes to the vibration symptoms operators report and the preventative measures that address the root cause.
| Failure Mode | Vibration / Operating Symptom | Root Cause | Preventative Measure |
|---|---|---|---|
| Step seal extrusion / nibbling | Loss of blow energy; erratic strike rhythm; oil weeping at the front head | Peak shock pressure exceeding the seal’s extrusion gap clearance | Use PTFE or hard-PU step seals with matched back-up rings; verify housing clearance during rebuild |
| Buffer seal fatigue | Increasing metal-on-metal knock; hammer overheating after short cycles | Repeated compression without recovery under strike frequency | Replace buffer and step seal as a set; specify high-recovery PU grades |
| Gas chamber charge loss | Gradual drop in striking power; hammer runs “soft”; no visible oil leak | O-ring compression set and nitrogen permeation | Fit FKM O-rings; verify static sealing during nitrogen recharge |
| Diaphragm cracking | Inconsistent energy per blow; pressure fluctuation in accumulator | Flex fatigue from continuous strike-frequency cycling | Select fatigue-rated diaphragm compound; replace on schedule not on failure |
| Wiper abrasion / contamination ingress | Premature wear of internal seals; scoring on the piston surface | Rock dust and fines bypassing a degraded wiper | Install heavy-duty wipers; improve front-head cleanliness and tool-lubrication practice |
| Decompression damage on O-rings | Blistering or splitting of static seals seen only on teardown | Rapid pressure release causing gas to expand within the elastomer | Specify materials with high decompression resistance; avoid trapped gas pockets |
Field note: When a breaker returns to the workshop with “low power” and no visible leak, the fault is frequently a gas chamber component rather than a dynamic seal. Pressure-testing the gas side before condemning the piston saves unnecessary teardown time and parts cost.
B2B Sourcing: Matching Specifications Before You Order
Breaker seal kits are model-specific. A kit that fits one hammer series will not fit another even when the bore diameter looks similar, because step seal profiles, groove widths, and buffer geometry vary by brand and generation. For B2B buyers, the sourcing workflow has three checkpoints: identify the exact hammer model and serial generation, confirm the original part numbers or measured cross-sections, and validate the material and hardness specification before committing to a batch.
Dimensional consistency is non-negotiable at the procurement stage. A sealing profile that is 0.1 mm outside tolerance may appear to fit but will leak, extrude, or fail to seat — a defect that surfaces at the customer, not at goods-in. Buyers should insist on documented dimensions and tolerance validation against the reference drawing for every batch, not just the first sample.
Batch Customisation, Volume, and Factory-Direct Supply
For distributors and repair chains, breaker seal kits are a consolidation opportunity. Rather than stocking dozens of single seals, a supplier that manufactures to order can build model-specific kits — combining step seal, buffer, O-rings, diaphragm, and wiper into one labelled pack per hammer model. Factory-direct production offers three B2B advantages:
- Batch customisation: kits assembled to your model coverage and packaging, with your labelling, so workshop staff pick one part number instead of eight.
- Consistent quality control: the same material source and moulds across batches, avoiding the drift that plagues mixed-source buying.
- Lead-time predictability: planned production runs aligned to your seasonal demolition and quarry demand.
When volumes justify tooling, custom profiles for a specific hammer series are economical and lock in fitment accuracy. The critical control is that customisation never bypasses inspection — a bespoke profile still has to pass the same dimensional and hardness gates as a catalogue part.
Procurement RFQ and Batch Quality Inspection Checklist
The table below is a practical RFQ and incoming-inspection template. Buyers can attach it directly to a purchase enquiry so that quotations are comparable and inspection criteria are agreed before the first shipment.
| Checkpoint | RFQ Requirement to Specify | Inspection Method / Acceptance Criterion |
|---|---|---|
| Dimensional tolerances | Quote measured cross-section, ID/OD, and groove width against the original part or drawing | Measure sample seals against the reference drawing; reject any batch outside the stated tolerance band |
| Material grade & hardness | State the polymer family (PU / PTFE / FKM / NBR) and target durometer for each component | Durometer (hardness) test on sampled seals; confirm batch certificate matches the specified Shore rating |
| Nitrogen sealing integrity | Confirm gas chamber O-ring and diaphragm suitability for charge retention | Pressure-hold / leak test on assembled gas chamber components; verify no charge loss over the test interval |
| Profile & geometry | Supply a profile drawing or reference sample for step seal and buffer seal | Visual and profile comparison against the reference; check lip angles and energiser seating |
| Batch traceability | Require batch/lot marking and a material declaration per shipment | Confirm lot code on packaging matches inspection records; retain a sample per batch |
| Packaging & kit labelling | Specify kit composition per hammer model and required labelling | Verify each kit contains the full component set and is labelled with the correct model reference |
Used consistently, this checklist turns quality from a post-mortem into a gate. A supplier comfortable with these requirements is usually one with real manufacturing depth rather than a trading intermediary.
Protecting Uptime: The Real Cost of a Breaker Seal Failure
The business case for premium breaker seal kits is best expressed in downtime, not unit price. A failed step seal on a production breaker can halt a demolition sequence or a quarry bench, and the replacement window is often longer than the workshop time because the machine has to be brought in. Factor in secondary damage — a leaking seal can allow contamination into the piston-cylinder interface, escalating a seal refresh into a piston or cylinder repair — and the low-cost generic kit stops looking cheap.
Procurement managers should therefore evaluate breaker seal kits on total cost of ownership: strike hours between rebuilds, repeat-failure rate, and the fitment accuracy that determines whether a rebuild goes right the first time. Kits that combine correct profiles, shock-rated materials, and batch-to-batch consistency reduce emergency orders and stabilise workshop scheduling.
Vetting Your Breaker Seal Supplier
Because so many breaker seals are sold through intermediaries, sourcing discipline matters as much as the specification. The indicators of genuine manufacturing strength are consistent across the industry: in-house moulding and material control, documented inspection records, the ability to produce custom profiles, and a willingness to be transparent about grades rather than substituting quietly. For a structured framework covering these signals, see this guide on vetting a hydraulic seal supplier. Applying those indicators to breaker kits specifically means asking whether the supplier can show durometer consistency, profile drawings, and gas-side leak-test data on request.
Frequently Asked Questions
How often should a breaker seal kit be replaced?
Replacement is best scheduled by strike hours and by function, not by waiting for failure. Dynamic components (step seal, buffer, wiper) typically set the interval, while gas chamber O-rings and diaphragms should be refreshed before they degrade striking power. Keeping a kit on hand for the model in service eliminates the lead-time penalty of an unplanned failure.
Can I replace only the leaking seal instead of the whole kit?
For breakers, no. Because the buffer seal and step seal share the shock load and the gas chamber components fail silently, replacing one seal leaves matched parts operating outside their design condition, which usually causes a repeat failure shortly after the rebuild.
Why does a premium seal kit cost more than a generic set?
The difference is in material grade, profile accuracy, and batch consistency — the three factors that determine how many strike hours you get per rebuild. A cheaper seal that fails early costs more in downtime, labour, and potential piston damage than it saves at purchase.
Do you supply custom breaker seal kits for specific hammer models?
Yes. Factory-direct production supports batch customisation to your model coverage, packaging, and labelling, with dimensional and hardness inspection applied to every batch. Buyers can share a profile drawing or a worn sample so the kit is built to the correct geometry.
Conclusion: Source Breaker Seals Like the Critical Part They Are
Hydraulic breaker hammer seal kits are consumables, but they behave like precision components. The combination of shock pressure spikes, high strike frequency, and nitrogen-backed gas sealing means the material, profile, and batch consistency of every component decide how long a hammer stays productive. For B2B buyers, the winning approach is straightforward: specify the exact hammer model, validate dimensions and tolerances against a reference, match materials to function, and inspect every batch against an agreed checklist.
Whether you are consolidating kits for a distributor network, standardising rebuild parts for a repair workshop, or keeping a quarry or demolition fleet running, the same controls apply. To discuss model coverage, batch customisation, and factory-direct supply for your breaker seal programme, reach out through our contact page and share your hammer models and volume requirements.
 Excavator Center Joint (Swivel Joint) Seal Kits: Internal Cross-Port Leakage Troubleshooting, PTFE Step-Seal Selection & B2B Overhaul Guide
 Excavator Main Control Valve Seal Kits: Spool Leakage Troubleshooting, Material Selection & B2B Sourcing Guide
 Motor Grader Hydraulic Cylinder Seal Kits: A B2B RFQ and Selection Guide
 Soft vs Metal-Backed Hydraulic Wiper Seals: A B2B Selection Guide for Replacement Kits